


HAIFEI chuan projection nut te chu electrical cabinet, equipment enclosure leh sheet{1}}metal assembly-a hman thin stainless-steel panel-a inzawmkhawmna tur capacitor discharge projection welding machine a siam a.
Machine hian welding cycle rei lo te chhungin electrical energy dahkhawm chu a chhuah tir thin. Dedicated positioning tooling leh controlled electrode force te nen hian nut joint him tak siam a pui a, chutih rualin panel discoloration, distortion leh nut misalignment te a tihtlem bawk.
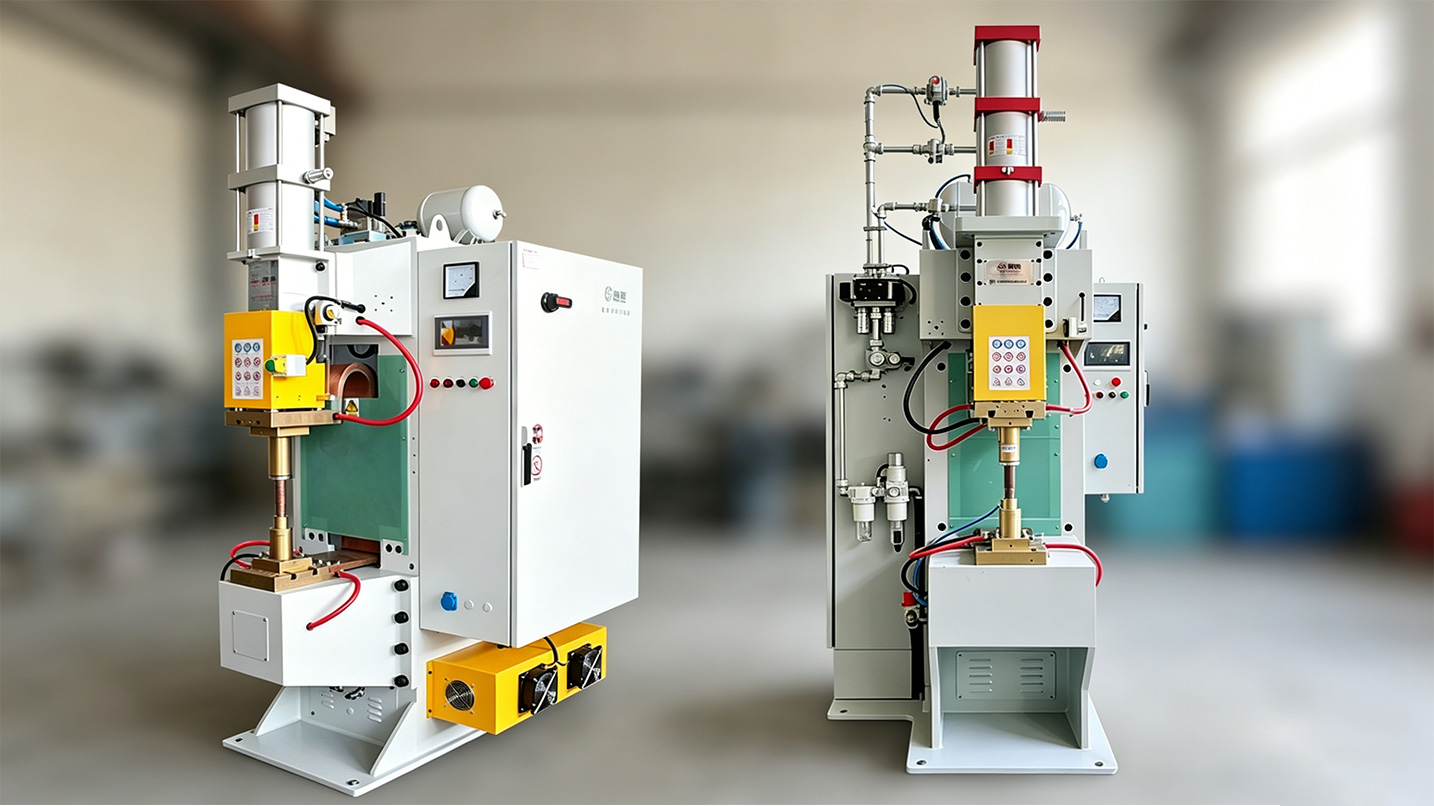
He Project atan hian eng Machine nge hman a nih?
He project atana hmanraw thlan chu stainless-steel panel leh nut siamna atana capacitor discharge projection welding machine bik a ni.
Machine hian electrical energy chu capacitor-ah a dahkhawm a, nut projection hmangin rang takin a chhuah tir thin. Panel pumpuiah zau taka hman ai chuan projection contact point-ah heat hi concentrate a ni.
He short energy-release cycle hi production problem chiang tak pathum chinfel nan thlan a ni a, chungte chu projection collapse tling lo, stainless-steel surface-a heat mark hmuh theih leh welded nut vel panel distortion te an ni.
Project Thupui tawi te
| Project Item a ni | Case chungchang hriat tur |
| Customer industry a ni | Voltage hniam-voltage electric hmanrua |
| Hnathawh tur thil | Stainless-steel panel leh projection nut hmanga siam a ni |
| Hmanrua | Capacitor atanga chhuak projection welding machine hmanga siam a ni |
| Welding hman dan | Nut projection hmanga siam a ni |
| Position siam dan tur | Centering leh locating fixture inhlan tak a ni |
| Ngaihtuah tur pawimawh ber | Joint chak lo, panel rawng danglam, distortion leh nut misalignment te |
| Product thlak danglam a ni | Tooling leh stored parameters te chu specification inmil tur atan |
| Validation a ni | Sample testing leh pre-delivery trial neih chhunzawm zel a ni |
Customer te chanchin
Customer chuan low-voltage electrical equipment atan stainless-steel sheet-metal parts, equipment enclosure leh a kaihhnawih assembly te a siam thin.
Cabinet assembly hmain projection nut te chu panel-ah weld a ngai a ni. Bolt dah lai hian nut siam zawh tawh chu a him reng a ngai a, a thread awmna erawh chuan bolt chu a luh theih nan a phal tur a ni.
Stainless-steel panel pawh hi enclosure chhunga hmuh theih a nih avangin, burn mark tam lutuk, yellowing, blackening emaw deformation emaw hian assembly leh appearance pahnih a nghawng thei a ni.
Engvangin Nge Process awmsa chu a nghet lo?
Welding hmasa ber khan nut projection-ah energy a concentrate tawk lo. Welding laiin projection thenkhat chu a insiam kim lo va, chu chuan joint chak lo emaw, kim lo emaw a siam a ni.
Chutih rual chuan, heat distribution inang lo chuan secondary problem engemaw zat a siam a:
| Production lama harsatna a awm | Finished Part-a nghawng a neih dan |
| Nut projection-a fusion tling lo | Nuts loose, joint kim lo emaw weld chhia emaw |
| Khua lum lutuk emaw, a inthlau lutuk emaw | Yellowing, blackening leh burn mark te a awm |
| Thermal contraction inang lo tak tak | Panel bulging, warping emaw edge distortion emaw a awm thei |
| Manual positioning tihsual a awm | Tilted emaw off-center nut emaw a awm thei |
| Energy output nghet lo tak a ni | Production cycle hrang hranga danglamna |
| Nut alignment tha lo tak a ni | Bolt jamming, cross-threading emaw, tightening inang lo emaw |
Heng harsatnate hi welding current tihpun chauhvin chinfel theih a ni lo. Energy tam zawk chuan nut position emaw pressure distribution emaw siamthat ngai lovin surface damage leh distortion a tipung thei a ni.
Customer-in Eng Nge A mamawh?
Customer chuan welding cycle rei lote chhunga nut projection siam thei tur leh a chhehvel panel chhunga lumna lut zat tihtlem thei tur process a mamawh a ni.
Nut position pawh a pawimawh ve tho. Fixture hian welding laiin centering, perpendicularity leh movement control a mamawh a, chutiang chuan a hnuaia assembly operation atan thread chu a align dik reng thei a ni.
He hmanrua hian nut size inmil leh stainless-steel panel thickness te pawh a support a ngai bawk. Welding parameters te chu repeat production leh nakin lawka process check na tur atan dahkhawm a ngai a ni.
Thil mamawh ber chu:
- Nut leh stainless-steel panel inkarah projection welding nghet takin dah rawh
- Yellowing tlem zawk, blackening leh hmuh theiha surface burning
- Panel bulging leh thermal distortion a tihziaawm
- Nut awmna leh alignment mumal tak
- Welding cycle inkara energy pek chhuah nghet tak
- Product specification inmil tur atan changeover awlsam zawk
- Welding recipe dahkhawm leh process traceability te

HAIFEI-in a chinfel dan tur a siam chhuah dan
Welding Trial te chu Actual Parts te nen
HAIFEI chuan machine an tihfel hmain customer-te stainless-steel material leh nut specification hrang hrang an test a.
Trial-te hi projection behavior, welding energy, electrode force, surface condition leh panel deformation te endikna atan hman a ni. Parameter te chu product tin tan general setting hmang lovin actual nut projection geometry angin an siamrem a ni.
Capacitor atanga chhuak tur projection Welding hmanga siam a ni
Hun rei lote chhunga energy dahkhawm tam tak pe chhuak thei tur capacitor discharge welding system thlan a ni.
Pressure kan pek chuan nut projection hrang hrangah current a kal tlang thin. Heng contact area tenau takah hian electrical resistance hian localized heat a siam a, chu chuan projection te chu a tichhia a, joint a siam thei a ni.
Heating cycle rei zawk nena khaikhin chuan he process hian nut chhehvela heat-a nghawngna hmun chu a tihtlem thei a ni. A remchan dan hi panel thickness, nut material, projection design, surface condition leh joint strength mamawh ah a la innghat tho.
Centering Fixture atana hman tur inhlan a ni
HAIFEI chuan stainless-steel panel leh projection nut siamna tur positioning tooling a design a.
Fixture hian part chu a zawng a, nut chu center-ah a dah a, welding pressure a pek laiin a hmunah a vawng tlat a ni. Uniform support hian projection collapse laiin movement leh uneven loading tihtlem nan a pui bawk.
He tooling hi hetiang hian ngaihtuah tur a siam a ni:
- Nut offset a ni
- Nut tilting a ni
- Electrode contact laiin chetna
- Projection-te chungah pressure inang lo tak a ni
- Welding hnua bolt alignment inmil lo
Machine khata nut specification inmil siam chhuah a nih chuan tooling insert hi tihdanglam theih a ni.
Controlled Pressure leh Stored Recipe te pawh a awm bawk
Welding energy chauh hian result a hril lo. Electrode force, contact condition leh timing te hian nut projection te a tlakchhiat dan a nghawng a ni.
Chuvangin machine hian clamping leh energy-release sequence chu a coordinate a ni. Setting pawm tawhte chu product recipe angin dah theih a ni a, hei hian repeat production-a manual adjustment a tihtlem phah a ni.
Final equipment configuration a zirin system hian recipe thlan, weld count, operating status leh alarm information te a record thei a ni. Data field leh communication interface mamawh te chu siam hmain confirm hmasa phawt tur a ni.
Engtin Nge Welding Cycle Hi A Hnathawh?
1
Operator chuan stainless-steel panel chu fixture chhungah a dah a.
2
Projection nut chu a mamawh hole chungah dah a ni.
3
Fixture hian components te chu a center a, a support bawk.
4
Welding head hian electrode force ruat sa chu a hmang a.
5
Capacitor te hian nut projection hmangin energy an chhuah tir thin.
6
Projection te chu an tlakbuak a, welded connection an siam ta a ni.
7
Welding head chu a rawn kir leh a, panel zawh tawh chu a chhuak ta a ni.
8
Joint chu pawm dan tur ruahman angin endik a ni.
Automated project tan chuan basic welding process validate a nih hnuah component feeding, part detection leh unloading te pawh dah belh theih a ni.
Engtin Nge Welded Nut hi Enfiah Tur?
Nut weld dik taka lang chu a la inmil lo thei a, mechanically a chak lo thei bawk. Acceptance plan hian joint, thread position leh panel condition te a huam tur a ni.
| Enfiah tur Item | Eng nge A Check |
| Mit hmuh theiha enfiah | Blackening, expulsion, burn mark leh surface chhiatna |
| Nut awmna hmun | Centering, perpendicularity leh thread alignment te a awm bawk |
| Bolt dahna tur test a ni | Jamming emaw cross{0}}threading emaw awm lovin engagement mumal tak |
| Push-out test a ni | Panel kaltlangin force hman laka do theihna |
| Torque test a ni | Tightening load tarlan tawh tuar thei |
| Peel emaw tihchhiatna test emaw | Projection siam dan leh inzawmkhawmna (joint integrity) a ni |
| Panel a flatness a awm | Bulging, warping leh local deformation te a awm bawk |
| Production trial chhunzawm zel a ni | Welding cycle a zawna tih leh theihna |
Original case hian pre-delivery trial chhunzawm zel laiin result nghet tak a report a, mahse numerical acceptance value erawh a tichhuak lo. Push-out force, torque, flatness leh appearance limits te hi customer in a supply tur a ni a, sample siam laiin a inrem tur a ni.
FAQ
Q: Stainless-steel panel-a nut weld nan eng machine nge hman?
A: He project ah hian capacitor discharge projection welding machine hman a ni a. Electrical energy dahkhawm chu nut projection kaltlangin welding cycle rei lo te chhungin a chhuak a, joint area-ah heat a concentrate a ni.
Q: Engvangin nge stainless steel atan capacitor discharge welding hi hman?
A: Discharge hun rei lote hian a chhehvel panel chhunga heat transfer tihtlem nan a pui thin. Hei hian nut projection, welding energy, electrode force leh tooling te dik taka inmil a nih chuan discoloration leh distortion a tihziaawm thei a ni.
Q: He process hian panel discoloration hi a veng vek thei ang em?
A: Eng process pawh hi application apiangah discoloration tihbo vek anga sawi tur a ni lo. Surface result hi stainless-steel grade, panel thickness, surface condition, projection design leh welding settings ah a innghat a ni. Sample test neih a ngai a ni.
Q: He machine hmang hian nut pangngai chu weld theih a ni em?
A: Projection welding atan hian a tlangpuiin welding projection tha tak tak neia design nut a ngai thin. Projection structure dik tak nei lo plain nut chuan joint design emaw process danglam tak a mamawh thei.
Q: Machine pakhat hian nut size engemaw zat a weld thei em?
A: Locating parts thlak theih leh stored recipe hmangin nut size inmil engemaw zat a support thei. Machine capacity, electrode access leh tooling space te hian product range kimchang a huam vek tur a ni.
Q: Engtin nge nut hi a tilt loh nan i ven?
A: Welding head-in pressure a pek hmain fixture hian nut chu a center a, a support bawk. Locating structure, electrode alignment leh uniform force te hian projection collapse laiin nut perpendicularity control nan a pui thin.